

To achieve an annual production scale of 450,000 tonnes of steel, the converter smelting capacity must be expanded, meaning the molten steel per heat must be increased from the current 100 t to 130 t or more. In line with the production requirements following the increase in converter capacity, this work designs a refractory lining repair and masonry scheme that enables a 100-tonne ladle to hold 130 tonnes of molten steel. The scheme must avoid causing slag overflow in the refining furnace due to excessive ladle charge, while also preventing a reduction in ladle campaign life and an increase in refractory material cost that would result from thinning the ladle working lining.
1.Calculation Method for Capacity Expansion
The ladle, an indispensable carrier in steelmaking production, serves as a key vessel for carrying molten steel and performing secondary metallurgy at the steelmaking–continuous casting interface. It organically links the various production processes together and ensures that steelmaking proceeds in an orderly manner. The ladle not only receives the molten steel tapped from the converter, but also acts as essential equipment for refining. While meeting the requirement of holding steel, it must also satisfy the refining process requirements, such as the freeboard requirement and the requirement for the upper inner diameter of the ladle. Therefore, the design and improvement of the 100-tonne ladle must ensure that its volume can accommodate the 130-tonne tapping output of the converter, while also adapting to the requirements of the refining process.
1.1 Main Design Parameters
(1) Main dimensions and process parameters of the 100-tonne ladle steel structure:
Top outer diameter: 3760 mm
Bottom outer diameter: 3280 mm
Total ladle height (excluding trunnion/leg brackets): 4065 mm
Freeboard above the molten steel surface: 400 mm
Liquid slag thickness: 150 mm
Specific gravity (density) of molten steel: 6.9 t/m³
(2) The ladle volume formula is given in Equation (1):

where:
H - ladle height, mm;
D - upper diameter of the ladle, mm;
D₁ - lower diameter of the ladle, mm.
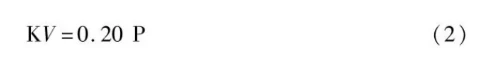
The revised formula is given in Equation (2):
where:
K - correction coefficient, with a value range of 0.93–0.96;
P - nominal capacity of the ladle, t.
1.2 Calculation Results
The ladle bottom is a relatively complex section, comprising the sliding system, the porous plug, the nozzle seat brick, and other components. On the premise of ensuring safe operation of the ladle bottom, this design adopts a castable ladle bottom to replace the brick-built ladle bottom. Theoretical calculation was carried out using the above parameters. The calculation shows that, to increase the molten steel capacity by 30 t based on the existing ladle, the inner diameter needs to be enlarged by 120 mm; in other words, the total refractory lining thickness of the ladle wall is reduced by 120 mm.
The new brick masonry scheme removes the 80 mm safety lining used for the ladle wall transition zone, as well as the 40 mm corundum self-flowing castable between the wall safety lining and the working lining.
This design does not reduce the thickness of the ladle permanent lining, and has no effect on the ladle shell (mould) dimensions. The existing ladle shell can continue to be used, while the dimensions and structure of all other sections remain unchanged.
2.Safe Masonry Process
2.1 Original Design Scheme and Masonry Process of the 100-Tonne Ladle
Ladle wall design:
Before ramming the permanent lining of the ladle wall, an insulation layer is adhered to the wall. The insulation layer is made of nano-scale thermal insulation material with a thickness of 10 mm. For ramming the permanent lining, the gap between the shell mould and the surrounding insulation panels is controlled within (100 ± 5) mm. The water addition during castable mixing is controlled at approximately 6.0%, with the flowability of the castable taken as the final criterion. After uniform mixing, the new ladle mould jig is placed in position. The ladle wall transition zone uses 80 mm insulation bricks; the ladle wall working lining uses 210 mm wall bricks, while the slag line section uses 240 mm magnesia-carbon bricks. A 40 mm corundum self-flowing castable is laid between the wall transition zone and the working lining. The height of the rim (brick edge) is required to be less than 120 mm.
Ladle bottom design:
First, a 100 mm permanent lining is rammed at the ladle bottom; the bottom is then repaired and masonried by combining a flat-laid bottom layer and a vertical-laid bottom layer. The porous plug seat brick and the nozzle seat brick are installed at the ladle bottom, with a reserved gap of 50–100 mm between these seat bricks and the bottom bricks. After the bottom bricks are laid, the gaps among the bottom bricks, the wall permanent lining, the nozzle seat brick and the porous plug seat brick are filled with corundum self-flowing castable. Bricks are then inserted and vibrated to achieve dense compaction, with brick joints staggered both longitudinally and transversely, fully filled with mortar. The ladle bottom is aligned, centered and firmly clamped during masonry; the finished bottom construction height is level with the porous plug seat brick, which can meet the operational requirements of a 400 mm freeboard and a 100 t ladle capacity.
2.2 Optimized Design Scheme and Masonry Process of the Ladle
Ladle wall design:
Based on the actual conditions at present, the scheme of expanding the ladle inner diameter by reducing the brickwork thickness is adopted to achieve capacity expansion. The 80 mm insulation bricks used in the wall transition zone are removed, and the 40 mm corundum self-flowing castable between the wall transition zone and the working lining is also removed. After ladle expansion, the rim bricks are eliminated and replaced by slag line bricks; otherwise the freeboard cannot meet the refining requirements. The calculation shows that, when the ladle freeboard is 400 mm, the ladle capacity reaches 132 t, meeting the optimized design requirements and the production demand for holding a 130 t molten steel charge. The original design scheme and the improved design scheme are shown in Figure 1.

Figure 1 Schematic diagram of the ladle design scheme
The ladle bottom is rammed with heavy-duty material and laid using a combination of flat-laid and vertical-laid masonry, with a thickness of 200 mm. The ladle bottom and nozzle seat brick still adopt the existing masonry method: the upper and lower seat bricks are installed first, and then the bottom bricks are laid up. When laying bricks, they must be tapped tight with a wooden mallet; the gap between bricks shall be less than 2 mm, with brick joints staggered longitudinally and transversely and fully filled with mortar. The bottom masonry is aligned, centered and firmly clamped. During major overhaul of the ladle, the bottom backing material must be re-rammed; during minor repair, when replacing the nozzle seat brick or the porous plug seat brick, the backing material must be rammed level with the porous plug seat brick.
2.3 Ladle Brick Optimization
The ladle wall bricks use 200 mm thick alumina-magnesia-carbon bricks, with the carbon content increased by 2%, i.e., a carbon content of 8%. The slag line bricks use 240 mm thick magnesia-carbon bricks, with the carbon content in the bricks increased by 2%, i.e., a carbon content of 14%, so as to improve the corrosion resistance of the bricks. The physical and chemical properties of the ladle bricks are given in Table 1.
| Item | MgO / % | C / % | Apparent porosity / % | Bulk density / (g·cm⁻³) | Cold crushing strength / MPa |
|---|---|---|---|---|---|
| Wall brick | 45 | 8 | ≤9 | ≥2.95 | ≥38 |
| Slag line brick | 76 | 14 | ≤5 | ≥2.98 | ≥35 |
Table 1 Physical and chemical properties of ladle bricks
3.Feasibility Verification of the Improved Ladle Scheme
3.1 Verification of the Ladle Center of Gravity and Trunnion Position
The trunnion position is of great importance for the entire ladle pouring process. If the trunnion position is too low, molten steel may be poured too quickly due to improper operation; if the trunnion position is too high, the overturning moment required during molten steel pouring will increase, which in turn raises the lifting load of the crane auxiliary hook and causes considerable energy waste. In ladle design, the trunnion center should be located 200–400 mm above the composite center of gravity of the ladle when fully filled with molten steel. The ladle center of gravity and trunnion position before and after modification are compared as follows.
(1) Coordinate origin: the midpoint of the trunnion connecting line.
(2) Center of gravity position before modification:
x=-2.569103mm
y=-352.736125mm
z=-4.602990mm
(3) Center of gravity position after modification:
x=-2.56900mm
y=-364mm
z=-4.52mm
The calculation results show that the ladle center of gravity and trunnion position meet the design requirements.
3.2 Ladle Overturning Moment Verification
During pouring, the overturning moment of the ladle consists of three parts: the overturning moment caused by the empty ladle, the friction moment at the ladle trunnions, and the overturning moment caused by the molten steel. By calculating the relationship between the lifting load of the crane auxiliary hook and the overturning angle, the lifting tonnage of the crane auxiliary hook is verified. The current 80 t auxiliary hook lifting load can fully meet the overturning requirements of the expanded ladle. It has been verified that this improved scheme does not affect the load-bearing capacity of ladle-related equipment such as the ladle car, the gantry hook and the continuous casting ladle turret; the relevant equipment requires no modification, and no additional cost is incurred for the ladle expansion modification.
3.3 Molten Steel Charge
Table 2 lists the converter tapping output for 20 heats each before and after ladle expansion. As can be seen from Table 2, through the adjustment and improvement of the ladle masonry process, the average converter tapping output of the 20 heats before expansion is 100.77 t, while that of the 20 heats after expansion is 130.93 t. The average converter tapping output has increased by about 30 t compared with before expansion, reaching the predetermined target.
| Before expansion Heat No. | Tapping output / t | After expansion Heat No. | Tapping output / t | Before expansion Heat No. | Tapping output / t | After expansion Heat No. | Tapping output / t |
|---|---|---|---|---|---|---|---|
| 22100023 | 99.3 | 22101012 | 130.3 | 22100033 | 100.2 | 22101022 | 129.1 |
| 22100024 | 99.5 | 22101013 | 131.2 | 22100034 | 98.9 | 22101023 | 131.3 |
| 22100025 | 101.2 | 22101014 | 132.5 | 22100035 | 99.8 | 22101024 | 133.8 |
| 22100026 | 99.2 | 22101015 | 130.6 | 22100036 | 102.2 | 22101025 | 128.1 |
| 22100027 | 102.3 | 22101016 | 135.4 | 22100037 | 101.8 | 22101026 | 129.1 |
| 22100028 | 102.4 | 22101017 | 133.5 | 22100038 | 102.3 | 22101027 | 128.2 |
| 22100029 | 100.6 | 22101018 | 129.2 | 22100039 | 98.4 | 22101028 | 131.2 |
| 22100030 | 102.1 | 22101019 | 128.3 | 22100040 | 101.5 | 22101029 | 132.6 |
| 22100031 | 100.5 | 22101020 | 130.5 | 22100041 | 99.9 | 22101030 | 133.3 |
| 22100032 | 102.1 | 22101021 | 131.1 | 22100042 | 101.2 | 22101031 | 129.3 |
Table 2 Comparison of converter tapping output before expansion (January 2022) and after expansion (February 2022) of the ladle
3.4 Ladle Temperature Drop
Although this design scheme removes the insulation bricks in the wall transition zone and reduces the insulation layer thickness, the castable offers the advantages of high apparent porosity, low bulk density, low thermal conductivity and small reheating shrinkage, providing good thermal insulation performance; therefore the ladle temperature drop remains normal. According to the production charts and data from February to May 2022, no molten steel was returned to the furnace due to excessive ladle temperature drop.
3.5 Ladle Campaign Life Comparison
From October 2021 to January 2022 before ladle expansion, the average ladle campaign life was 115.45 heats, with a refining ratio of 28.92%. After the expansion and optimization, from February to May 2022, the average ladle campaign life was 116.31 heats, with a refining ratio of 29.77%. The ladle operated steadily, with no noticeable adverse impact.
4.Conclusions
By changing the refractory brick material of the ladle and redesigning the safe masonry method, the predetermined target of expanding the 100 t converter ladle by 30 t has been achieved, effectively promoting the increase in steelmaking output and steel production. The scheme is now being promoted and applied.
(1) Through the optimized design and improvement of the 100 t ladle, the improved ladle fully meets the requirement of holding 130 t of molten steel, without exceeding the load-bearing capacity of the 240 t crane.
(2) The original 100 t ladle used a total of 54.7 t of refractory material; after the improved design, the refractory consumption of the ladle was reduced to 40.2 t. On the basis of ensuring safe ladle operation, the refractory cost per tonne of steel was lowered. Meanwhile, as the output per heat increased, the energy cost and labor cost per tonne of steel decreased accordingly, effectively reducing the production cost per tonne of steel.
(3) This design scheme enlarges the effective volume of the ladle and increases the molten steel charge, while also increasing the ladle freeboard, which helps avoid slag overflow in the refining furnace and ensures the effective space required for LF refining of molten steel. It is of great significance for achieving effective secondary refining of molten steel, improving steel quality, upgrading product grades and increasing the proportion of premium grades.