

1 . Analysis of the Causes of Flue Gas Leakage through Kiln Wall in Calcining Zone of Lime Kiln
In the soda ash production system, the vertical lime kiln is mainly composed of two layers of refractory bricks, or two layers of refractory bricks plus one layer of insulating bricks and aluminum silicate boards on the kiln interior, with kiln shell steel plates of varying thicknesses on the outermost side. During the calcination of limestone inside the kiln, three zones are formed sequentially from top to bottom along the kiln height: preheating zone, calcining zone and cooling zone. The calcining zone accounts for half of the kiln height, and the calcination temperature is generally controlled at 1150~1200℃.
When limestone contains high impurities, ring accretion will form in the calcining zone. As the lime kiln approaches its major overhaul cycle, the bonding strength of mortar for refractory bricks inside the kiln decreases. If large accretion lumps adhere to the kiln wall, they may cause the inner and outer refractory bricks to fall off as the lumps descend together with materials. The transverse and vertical brick joints of inner and outer refractory bricks are staggered during masonry. Missing refractory bricks will allow high-temperature flame in the calcining zone to spread outward through the brick voids. Meanwhile, the temperature in the calcining zone exceeds 1000℃. With CaO as the main component derived from limestone, refractory bricks are susceptible to alkaline attack, leading to damage of inner refractory lining. Excessive verticality deviation and horizontal radius deviation during masonry of inner refractory bricks also cause premature failure of calcining zone refractory bricks and result in flame leakage through the kiln wall.
2 . Exploration of On-line Repair Methods for Inner Lining of Lime Kiln
A full kiln shutdown for re-masonry of refractory bricks takes a long time. In cases where the kiln has not reached its overhaul cycle and production cannot afford shutdown, on-line repair is required to address the flame leakage issue described above. Based on the structural features of the lime kiln and the special properties of inner refractory bricks, two on-line repair methods for inner refractory lining have been proposed and applied on site.
2.1 External Box Attachment Method on Kiln Wall
Taking a lime kiln with an outer diameter of 6860 mm as an example, Q355B low-alloy high-strength structural steel with yield strength ≥355 MPa and tensile strength of 470–630 MPa is adopted for the external box. This grade guarantees overall structural strength, good weldability, and easy processing for cutting, bending and stamping. Prefabricate components as follows: one curved plate of 10 mm thick Q355B steel with radius of 3630 mm, arc length of 3000 mm and height of 3000 mm; two side plates sized 3000 mm × 200 mm; one upper and one lower annular plate each with radius of 3430 mm and width of 200 mm; ten isosceles right triangular stiffener plates with side length of 200 mm.
Detailed repair procedures are listed below:
① Weld prefabricated lower annular plate and side plates onto the outer surface of the kiln shell.
② Weld 5 triangular stiffener plates beneath the lower annular plate.
③ Lay LZ-70 refractory bricks within the area bounded by the lower annular plate and side plates. All brick joints shall be filled with mortar containing Al₂O₃ ≥65%.
④ Apply an even layer of mortar over the outer surface of the laid refractory bricks after masonry completion.
⑤ Use adhesive to bond two layers of aluminum silicate boards onto the mortar layer on refractory bricks. The aluminum silicate board has bulk density of (150±10) kg/m³, Al₂O₃ ≥45%, thermal conductivity ≤0.153 W/(m·K), and long-term service temperature of 1150℃.
⑥ Press the prefabricated curved plate against the aluminum silicate boards and perform full penetration welding to connect it with the lower annular
plate and side plates, ensuring no gaps between aluminum silicate boards and the mortar layer on refractory bricks.
⑦ Fully weld the prefabricated upper annular plate to the kiln shell, side plates and curved plate.
⑧ Weld 5 triangular stiffener plates above the upper annular plate.
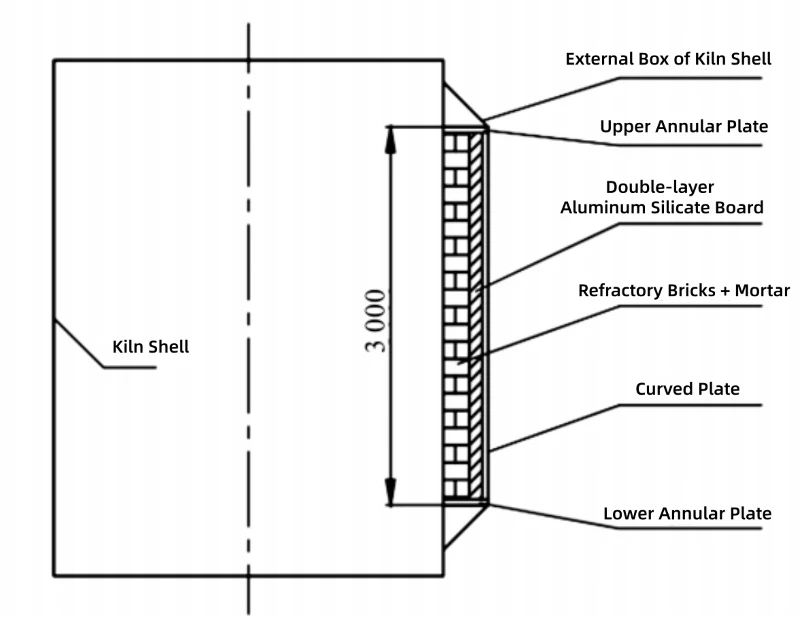
Figure 1 External Box Attachment Method on Kiln Wall
2.2 Method of Injecting High-temperature Resistant Castable into Kiln Wall
When the damaged area of refractory bricks in the calcining zone is excessively large, the overall supporting strength for the refractory bricks in the upper preheating zone will be lost. There is a risk of large-area collapse during lime kiln operation. Therefore, high-temperature resistant castable needs to be poured into the refractory brick layer of the lime kiln to fill the eroded and missing refractory bricks and improve the overall strength of the kiln lining. Taking an erosion area of 1500 mm (height) × 2200 mm (arc length) as an example, the specific repair procedures are as follows:
① Weld gantry guide frames on the kiln wall: Weld gantry guide frames upward with the horizontal elevation of the detected erosion area as the boundary. The spacing between adjacent gantry guide frames shall not exceed 300 mm, and the uppermost guide frame shall not go beyond the upper edge of the erosion zone. The frames are used to fix the pins inserted from outside the kiln wall and ensure that the pins are perpendicular to the kiln wall. It is estimated that five rows of guide frames need to be welded.
② Support by inserting pins: Drill holes on the kiln wall corresponding to the guide holes of all gantry frames. Drive pins into the kiln through the guide holes on the gantry frames and the holes in the kiln wall. The penetration depth shall be no less than 800 mm, and the spacing between adjacent pins shall not exceed 150 mm. The pins are used to support the ash layer above them, preventing massive collapse and outflow of upper ash and stone blocks during hole cleaning in the lower section, which may cause personal injury.
③ Hole cleaning for the first layer: After all supporting pins are driven in, drill holes sequentially from bottom to top and from east to west at the bottom of the erosion area. The size of a single hole shall not exceed 500 mm (width) × 200 mm (height). After drilling, use prefabricated hooks to pull out internal ash, stone blocks and loose refractory bricks on both sides. Clean the bottommost refractory bricks to form a flat horizontal surface, with an excavation depth of about 800 mm until a sound and intact refractory brick surface is exposed. Repeat the above process to thoroughly clean the interior of the whole area. During hole opening, at least 2 strips of kiln shell plate with sufficient width shall be reserved longitudinally in the entire erosion zone to guarantee the overall strength of the holed area.
④ Formwork erection for the first layer: After cleaning, erect carbon steel formwork vertically close to the ash blocks. Make the outer arc of the formwork flush with the inner surface of the existing refractory bricks as much as possible.
⑤ Restoration of the first layer holes: Use round steel to make hooked rebars, weld them to the inner side of the cut first-layer steel plate, then weld the steel plate with hooked rebars at the hole position to enhance the overall stability of the castable.
⑥ Hole cleaning for the second layer: Repeat the hole cleaning procedures for the first layer, and re-clean the area below the second row of pin supports.
⑦ Casting of castable for the first layer: Pour pre-mixed castable into the kiln through the second-layer square holes. Stop pouring when the castable is 50 mm away from the first row of pins. Use a vibrator to compact and homogenize the castable during pouring to reduce voids inside.
⑧ Remove the first row of pins: Extract the first row of pins and gantry frames one by one.
⑨ Inspection of refractory bricks: Repeat the above maintenance steps until the area below the fourth row of pins is cleaned. Drill an inspection hole at the upper edge of the erosion zone; the inspection hole shall be no larger than 200 mm (height) × 500 mm (width). Drill holes from east to west and from bottom to top. Clean refractory bricks from outside to inside after hole opening, inspect the brick condition, and find the elevation where all three layers of refractory bricks remain intact without falling off.
⑩ Support by inserting pins: Drive pins into the kiln closely against the lower edge of the refractory bricks. The penetration depth shall be no less than 800 mm, the spacing between adjacent pins shall not exceed 150 mm. At least 200 mm of each pin shall be reserved outside the kiln, and fixed to the upper kiln wall with stiffener plates, to prevent collapse and outflow of refractory bricks and ash blocks which may cause personal injury.
⑪ Hole cleaning: Perform hole cleaning construction in accordance with Step 3).
⑫ Formwork erection: After cleaning, erect carbon steel formwork vertically close to the ash blocks. Make the outer arc of the formwork flush with the inner surface of the existing refractory bricks as much as possible.
⑬ Remove the fourth row of pins: After the fifth layer is cleaned, extract the fourth row of pins and gantry frames one by one.
⑭ Casting of castable: Uniformly drill 3 square holes above the fifth row of pins. Pour castable through the square holes to fill the gap above the refractory bricks and around the fifth row of pins. Cut off the portions of the fifth-row pins protruding outside the kiln wall.
⑮ A vibrator must be used to compact and homogenize the castable after casting of each layer to reduce voids in the castable.
Due to the large number of construction steps above, Figure 2 only illustrates the main construction procedures.
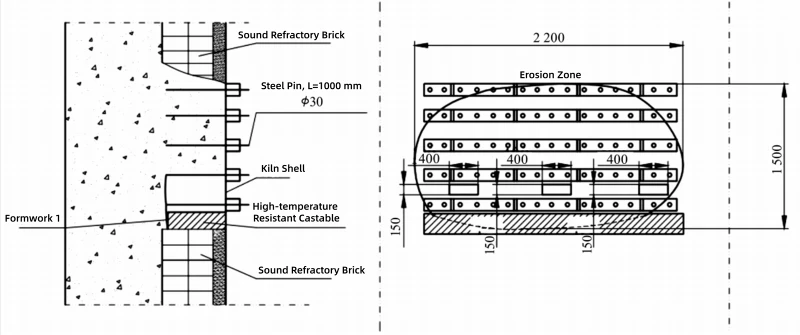
Figure 2 Hole Opening and Castable Pouring
3 . Summary of Repair Methods
The external kiln shell box attachment method features high repair efficiency and low risk factor. However, if the repair area exceeds 20 m², it will exert a certain impact on the overall wind resistance of the lime kiln. The method of injecting high-temperature resistant castable into the kiln wall is applicable to large-area kiln wall repair, yet it requires a long maintenance period.
The above two repair methods can be reasonably selected according to actual site conditions. They can effectively prevent flame leakage through the kiln wall caused by damaged refractory bricks in the calcining zone of the lime kiln, and effectively extend the service life of the equipment. It avoids the need for standalone major overhaul triggered by damage to the inner refractory lining. In addition, these two repair methods can also be adopted to address flame leakage in other parts of the lime kiln arising from the same causes.